


Phone:
+86-138-0577-0261


Views: 0 Author: Site Editor Publish Time: 2026-09-18 Origin: Site


Hermetic sealing is the critical failure point in food packaging. A compromised seal leads to spoilage, recalls, and damaged brand reputation, regardless of the quality of the food inside. Food manufacturers and packaging engineers must balance seal integrity, production throughput, and material compatibility. You specifically need to match lidding films to Polyethylene Terephthalate (PET) substrates without warping the container or causing micro-leaks. This guide breaks down the technical mechanics of sealing a PET container. We compare primary sealing technologies like Heat, MAP, VSP, and Ultrasonic. We also provide a framework for evaluating sealing machinery based on scalability, vendor support, and compliance requirements. You will learn how to optimize your production line, reduce material waste, and ensure every package leaving your facility meets strict food safety standards.
Polyethylene Terephthalate dominates the food packaging sector because it offers excellent clarity, robust barrier properties, and high mechanical strength. However, you cannot treat all PET formulations the same way on the production line. Understanding the thermal properties of your specific substrate is the first step in achieving a hermetic seal. When you set up a production run for a plastic tray, you must first verify whether you are working with Amorphous PET (APET), Crystallized PET (CPET), or Recycled PET (rPET).
APET is the industry standard for chilled and ambient applications. It provides glass-like clarity, allowing consumers to inspect the product before purchase. The operational challenge with APET is its relatively low glass transition temperature, which hovers around 70°C (158°F). If your sealing platen applies excessive heat, or if the dwell time is too long, the flange will distort. This warping compromises the structural integrity of the container and creates microscopic gaps where the lidding film fails to bond.
CPET undergoes a crystallization process during manufacturing that turns the material opaque and drastically increases its thermal resistance. Facilities use CPET primarily for dual-ovenable ready meals because it withstands temperatures up to 220°C (428°F). Because CPET resists heat deformation, it requires entirely different sealing parameters. You must run your platens at much higher temperatures to activate the lidding film's sealant layer without worrying about melting the rigid structure beneath it.
rPET introduces another variable. While it offers significant sustainability benefits, the inclusion of post-consumer recycled content can sometimes lead to slight variations in material thickness and thermal behavior. Operators running rPET often need to monitor their sealing parameters more closely, making micro-adjustments to pressure and temperature throughout the shift to maintain a consistent bond.
| Material Type | Visual Appearance | Thermal Resistance | Primary Application |
|---|---|---|---|
| APET | High Clarity / Transparent | Up to 70°C (158°F) | Fresh produce, cold deli meats, bakery |
| CPET | Opaque / Colored | Up to 220°C (428°F) | Microwave and oven-ready meals |
| rPET | Clear to slightly tinted | Up to 70°C (158°F) | Eco-friendly packaging, ambient goods |
A successful seal relies entirely on the engineered compatibility between the flange and the lidding film. You cannot simply buy generic plastic film and expect it to bond with a specialized substrate. Modern lidding films are complex, multi-layer extrusions designed to perform several functions simultaneously. The outer carrier layer, usually made of heat-resistant polyester, prevents the film from melting onto your heated sealing platen. Beneath this sits the barrier layer. Facilities frequently utilize Ethylene Vinyl Alcohol (EVOH) in this layer to block oxygen ingress, which is mandatory for preserving freshness in perishable goods.
The innermost layer is the sealant layer. This specific polymer blend must chemically and thermally bond with the flange. Packaging engineers must specify whether an application requires a peelable seal or a weld seal. A weld seal, also known as a lock-seal, permanently fuses the film to the flange. We use this approach to secure liquid-heavy products during transit, ensuring the package will not burst if dropped. An easy-peel seal relies on a cohesive failure mechanism engineered directly into the sealant layer. When the consumer pulls the film, the layer separates cleanly without requiring knives or scissors.
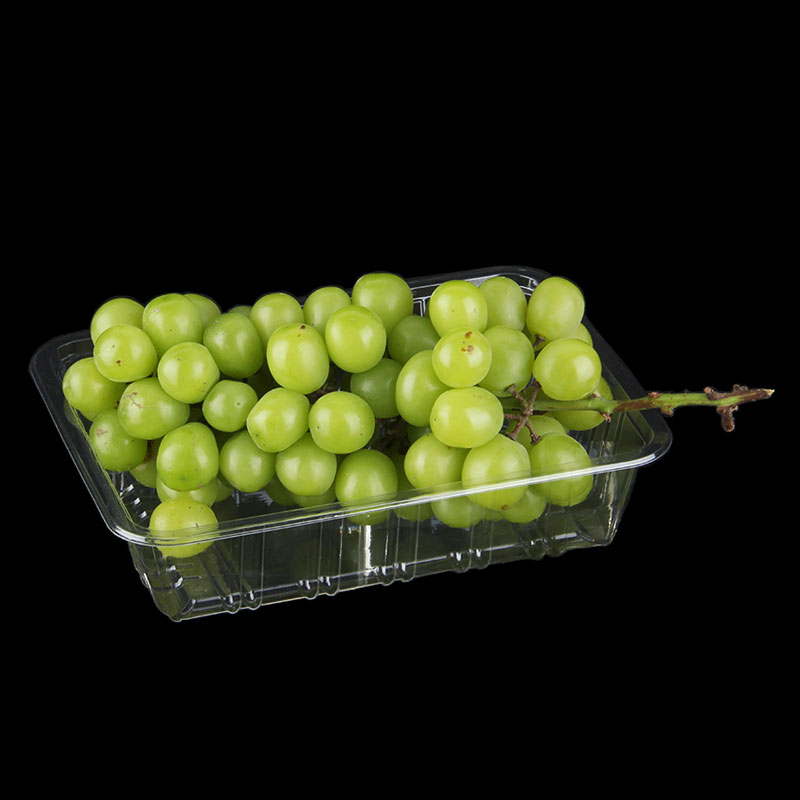
Advanced film treatments also play a massive role in product presentation and functionality. Anti-fog coatings are heavily utilized to alter the surface tension of the film. When moisture evaporates from the food, this coating forces the water to form a thin, transparent sheet rather than opaque condensation droplets. This treatment is absolutely essential for maintaining clear product visibility when utilizing a recyclable PET fruit tray stored in fluctuating refrigerated environments. Without anti-fog properties, the package looks cloudy and unappealing on the retail shelf.
The fundamental physics of heat sealing are governed by the Sealing Triangle: dwell time, platen temperature, and mechanical pressure. You must calibrate these three variables perfectly to achieve a flawless hermetic bond. Temperature provides the thermal energy required to melt the sealant layer, allowing it to flow into the microscopic imperfections of the flange. If the temperature is too low, the bond remains weak and easily breached. If it is too high, the film burns, or the flange warps.
Dwell time refers to the exact duration the heated platen remains in contact with the film and flange. High-speed production lines naturally demand shorter dwell times to maintain throughput. To compensate for this reduced time, operators must incrementally increase the temperature or pressure. Mechanical pressure ensures uniform contact across the entire perimeter of the seal. Uneven pressure distribution, often caused by worn tooling or misaligned platens, results in localized weak spots.
Follow these steps to calibrate your sealing machine for a new production run:
Conduction heat sealing remains the most widely deployed technology in the food packaging sector due to its reliability and mechanical simplicity. The mechanism involves a heated metal platen pressing the lidding film directly against the supported flange. The thermal energy transfers through the film's carrier layer, melting the sealant layer and fusing it to the substrate. This method is highly efficient for high-speed operations where atmospheric modification is unnecessary.
This technology is best suited for short-shelf-life products, ambient dry goods, and standard delivery applications. A standard food delivery tray usually only requires a basic conduction seal because the primary goal is physical protection and spill prevention during a brief transit window. The equipment is relatively inexpensive to maintain, requiring only routine replacement of Teflon tape on the platens and periodic checks of the pneumatic cylinders that drive the sealing head.
However, standard conduction sealing has distinct limitations regarding preservation. Because it simply traps the ambient factory air inside the package, it offers no active shelf-life extension. Products prone to rapid oxidation or microbial growth will still degrade at their natural rate. You cannot use standard conduction sealing for highly perishable raw proteins or fresh-cut produce that require extended distribution cycles across multiple state lines.
Modified Atmosphere Packaging fundamentally alters the internal environment of the sealed container to drastically slow down biochemical degradation and microbial spoilage. The mechanical process is complex. Before the heated platen descends to seal the film, the machine pulls a deep vacuum to evacuate the ambient oxygen from the chamber. Immediately following the vacuum cycle, the manifold flushes the chamber with a precisely calibrated mixture of gases before the final seal is applied.
If you are packaging raw meat or fresh pasta in a supermarket fresh tray, MAP is non-negotiable. Different foods require vastly different gas ratios. Raw red meats often utilize high oxygen levels to maintain a desirable bright red color through myoglobin oxidation. Conversely, fresh pastas and baked goods rely on high carbon dioxide and nitrogen blends to inhibit mold growth and prevent the package from collapsing as the product absorbs gases over time.
Implementing MAP requires specialized high-barrier materials and EVOH-equipped lidding films to prevent the protective gases from escaping. The machinery itself requires heavy-duty vacuum pumps, precision gas mixers, and specialized hermetic tooling. While the capital investment is significant, the resulting shelf-life extension allows manufacturers to distribute products nationally rather than just locally.
| Food Product | Oxygen (O2) % | Carbon Dioxide (CO2) % | Nitrogen (N2) % | Primary Preservation Goal |
|---|---|---|---|---|
| Raw Red Meat | 70 - 80% | 20 - 30% | 0% | Maintain red color, inhibit anaerobic bacteria |
| Fresh Pasta | 0% | 50 - 60% | 40 - 50% | Prevent mold growth, prevent package collapse |
| Hard Cheese | 0% | 100% | 0% | Stop mold formation completely |
| Cooked Meats | 0% | 20 - 30% | 70 - 80% | Prevent oxidation and rancidity |
Vacuum Skin Packaging offers premium presentation and exceptional preservation by completely eliminating the headspace within the package. In a VSP machine, a highly flexible, formable lidding film is heated inside a vacuum chamber until it reaches a softened, drapeable state. The machine then pulls a vacuum from beneath the container, causing the heated film to drape tightly over the contours of the food product and fuse completely to all exposed areas of the flange and interior walls.
This second skin effect locks the product in place. It prevents liquid migration and purge, which is particularly beneficial for premium cuts of meat, marinated proteins, and high-end seafood. The total elimination of oxygen drastically extends shelf life while providing a visually striking, three-dimensional presentation on retail shelves. Consumers can inspect the product from multiple angles without liquid sloshing around inside the package.
The primary engineering consideration for VSP is structural rigidity. The underlying container must possess sufficient mechanical strength to withstand the intense vacuum forces without buckling, warping, or collapsing during the sealing cycle. You must source specifically designed rigid substrates with reinforced sidewalls to handle the stress of the VSP process.
Ultrasonic sealing represents a highly advanced alternative to traditional thermal conduction. Instead of relying on external heating elements, this technology utilizes high-frequency acoustic vibrations—typically between 20 kHz and 40 kHz—generated by a titanium horn known as a sonotrode. When the machine applies these vibrations to the film and flange under pressure, they create intense internal molecular friction within the plastic polymers. This friction generates localized heat precisely at the seal interface, melting the materials together in a fraction of a second.
The most significant advantage of ultrasonic sealing is its ability to seal through contamination. If liquid, grease, or small food particles spill onto the flange during the filling process, the high-frequency vibrations effectively push the contaminants out of the seal zone before the polymer fuses. This capability drastically reduces false rejects and minimizes material waste.
Facilities processing leafy greens, liquid soups, or heavy sauces frequently deploy ultrasonic systems. In these messy production environments, traditional heat seals would fail constantly due to channel leaks caused by debris. Ultrasonic technology ensures hermetic integrity even when the filling nozzles drip or splash product onto the sealing surfaces.
Selecting the appropriate sealing machinery requires a rigorous assessment of your current production volumes and anticipated growth. Manual or tabletop sealers represent the entry point. These units typically process under 300 units per hour. They require an operator to manually load the container, pull the film across the top, and pull a lever to initiate the sealing cycle. We recommend these machines for pilot testing, recipe development, or low-volume localized delivery operations where you need to minimize capital expenditure.
Semi-automatic shuttle sealers bridge the gap for medium-volume facilities. Operators still load the containers into a sliding drawer or rotary table, but the machine fully automates the film feeding, gas flushing, sealing, and cutting cycles. These machines can typically handle between 10 and 20 cycles per minute, depending on the vacuum requirements.
For high-volume industrial environments producing thousands of units per hour, fully automatic inline sealers are mandatory. These robust systems utilize servo-driven walking beams or continuous motion conveyors to index containers through the sealing station without human intervention. They maximize throughput and ensure absolute consistency across multiple shifts, easily achieving speeds exceeding 100 trays per minute on multi-lane configurations.
An inline sealer does not operate in isolation. It must function as a seamless component within a broader automated packaging ecosystem. Advanced sealing equipment utilizes Programmable Logic Controllers (PLCs) to communicate continuously with upstream and downstream machinery. Upstream integration involves synchronizing the sealer's indexing speed with automated denesters, which drop the empty containers onto the conveyor, and volumetric filling stations. If the filler misses a container, the PLC must tell the sealer to skip that specific lane to prevent sealing an empty package.
Downstream compatibility is equally critical for quality assurance and logistics. Once the package exits the sealing chamber, the system must facilitate smooth hand-offs to dynamic checkweighers. These scales verify product fill limits and automatically reject under-filled or over-filled units. Integration with metal detectors or X-ray inspection systems ensures foreign body detection. Finally, automated print-and-apply labeling machines require precise spacing and orientation of the sealed packages as they move toward end-of-line case packing and palletizing operations.
Production agility heavily depends on the engineering of the machine's sealing dies and tooling plates. Facilities rarely run a single package format continuously. Operators must frequently switch from sealing deep, multi-compartment deli containers to shallow, single-serve formats within the same shift. The speed and simplicity of these format changeovers directly impact your overall equipment effectiveness and operational profitability.
Evaluate machinery based on tool-less changeover capabilities. Modern systems utilize quick-release mechanisms and RFID-tagged tooling that automatically updates the machine's PLC recipes. Pre-heated docking stations eliminate the warm-up time associated with swapping heavy metal platens. When an operator slides a new hot plate into the machine, it is already at the target temperature, allowing production to resume immediately.
Operations managers must also weigh the initial investment of custom-machined tooling plates tailored to proprietary package shapes against the flexibility of adjustable, universal plates. Universal plates can accommodate standard industry footprints with minimal adjustment, saving thousands of dollars in tooling costs if you frequently run short batches of varying sizes.
Film handling mechanisms significantly influence both aesthetic quality and material consumption. Standard straight-cutting systems slice the film in a continuous grid, leaving sharp, square corners that overhang the rounded edges of the flange. While mechanically simple and cheap to maintain, this method results in an unrefined appearance and potential handling issues during retail display, as the sharp corners can snag on adjacent packages.
Profile cutting utilizes precision-machined blades to cut the film exactly along the perimeter of the flange, resulting in a clean, flush finish. Managing the skeletal film waste—the excess material left over after profile cutting—requires robust rewind systems. Servo-driven tension controllers ensure the waste web is pulled smoothly without snapping. If the skeletal web snaps, it causes immediate line stoppages and requires an operator to re-thread the machine.
Advanced machinery optimizes the film advance pitch, minimizing the gap between consecutive cuts to reduce raw material waste. Over millions of cycles, optimizing film tension and reducing the advance pitch by just a few millimeters yields substantial reductions in consumable expenditures.
Even with highly calibrated equipment, seal failures occur, leading to rapid product degradation. Channel leaks are the most prevalent issue. They are typically caused by organic debris, grease, or moisture contaminating the flange prior to sealing. When the heated platen descends, it fails to bond the film through the debris, creating a microscopic tunnel where oxygen enters and protective gases escape. Mitigating channel leaks requires optimizing upstream filling nozzles to prevent dripping or implementing mechanical flange-wiping brushes.
Film curling and flange warping are generally symptoms of thermal mismanagement. Applying excessive heat or prolonged dwell time to a standard APET substrate causes the polymer memory to react, warping the structural geometry of the container. Weak or inconsistent seals often stem from incompatible sealant layers, degraded Teflon coatings on the heating platen, or uneven mechanical pressure across the die face.
Use this troubleshooting checklist when encountering weak seals:
Validating hermetic integrity requires a combination of destructive and non-destructive testing protocols. Destructive testing involves sacrificing a statistical sample of the production run to quantify mechanical strength. Burst testing introduces pressurized air into the sealed package through a needle until the seal ruptures. This provides measurable data on the exact pressure threshold the bond can withstand. Tensile peel testing utilizes laboratory equipment to measure the exact force required to separate the film from the flange, ensuring the seal meets the specified parameters for either secure transport or easy-peel consumer access.
Non-destructive testing is deployed for high-speed, inline quality assurance without generating product waste. Vacuum decay systems place the sealed package inside a specialized testing chamber. The chamber draws a vacuum, and highly sensitive transducers monitor for minute pressure changes that indicate gas escaping from a micro-leak in the package.
Additionally, high-resolution vision inspection systems utilize specialized lighting and cameras to scan the perimeter of every single package. These systems instantly detect visual defects, wrinkles, or trapped food particles in the seal zone. If the software identifies a flaw, it triggers a pneumatic reject arm to automatically push the compromised unit off the line before it reaches the case packer.
Packaging materials in direct contact with food are subject to stringent regulatory frameworks governing chemical safety and consumer protection. A critical compliance metric is managing migration limits. Under specific conditions—such as high heat during microwave use for CPET containers or prolonged exposure to highly acidic foods—chemical compounds from the sealant layer or the plastic substrate can potentially leach into the consumable product.
Packaging engineers must source materials backed by comprehensive documentation proving compliance with FDA, EFSA, or regional regulatory standards regarding overall migration limits (OML) and specific migration limits (SML). You cannot assume a film is safe for all applications just because it is food-grade.
Furthermore, facilities must maintain rigorous traceability protocols. You must document the exact lot numbers of films and rigid substrates used during specific production runs. This data ensures that in the event of a material defect or safety anomaly, your operation can execute precise, targeted recalls rather than catastrophic, facility-wide product withdrawals. Integrating your sealing equipment's PLC data with your facility's ERP system automates this traceability, logging the exact parameters and material lots for every batch produced.
A: The optimal sealing temperature for APET typically ranges between 130°C and 160°C (266°F to 320°F), depending on the specific lidding film and machine dwell time. Exceeding these temperatures risks warping the flange or shrinking the container, as APET has a relatively low glass transition temperature.
A: Generally, no. Standard conduction heat sealers lack the heavy-duty vacuum chambers, gas mixing manifolds, and specialized hermetic tooling required to evacuate ambient air and flush the package with modified gas mixtures. MAP requires purpose-built machinery designed to handle deep vacuums and pressurized gases.
A: Film curling is usually caused by excessive heat application or a mismatch in the thermal shrinkage rates between the multi-layer film and the rigid substrate. Lowering the platen temperature, reducing dwell time, or switching to a film with better dimensional stability under heat resolves this issue.
A: Ultrasonic sealing uses high-frequency acoustic vibrations to generate internal molecular friction. This intense, localized vibration physically pushes liquid, grease, and small food particles out of the seal zone just milliseconds before the polymer layers melt and fuse together, ensuring a clean bond.
A: A lock-seal, or weld seal, permanently fuses the film to the substrate. It requires a knife or scissors to open, making it ideal for heavy or liquid products. An easy-peel seal is engineered to separate cleanly with manual pulling, prioritizing consumer convenience without sacrificing hermetic integrity.
A: Best practices dictate performing destructive testing at the start of every shift, immediately following any tooling changeover, and after any adjustments to the temperature, time, or pressure settings on the machine's control panel. This ensures the seal parameters remain within acceptable tolerances.


