


Phone:
+86-138-0577-0261


Views: 0 Author: Site Editor Publish Time: 2026-09-17 Origin: Site


Food distributors, retailers, and agricultural suppliers face intense pressure to meet strict sustainability mandates while maintaining food safety, shelf life, and visual appeal. You need packaging that protects highly perishable goods during transit but does not end up in a landfill. The core problem lies in the massive gap between theoretical material recyclability and actual municipal recycling capabilities, specifically regarding Polyethylene Terephthalate (PET) packaging. A container might be technically recyclable in a laboratory setting, but its journey through local waste management infrastructure often yields a completely different outcome.
We will evaluate PET packaging using a comprehensive framework focused on material science, local recycling infrastructure realities, regulatory compliance, and overall procurement value. Understanding the exact mechanical and chemical properties that dictate whether a container is recovered or rejected is necessary for building a resilient and compliant packaging strategy.
Polyethylene Terephthalate (PET) dominates the fresh food packaging industry for specific mechanical reasons. We use it because it offers unparalleled optical clarity. Consumers want to inspect fresh produce directly on the shelf without opening the package. PET also delivers high shatter resistance. When you stack pallets of berries or tomatoes, the bottom layers take a beating. PET ensures the containers survive the impacts of transit, forklift handling, and retail stocking. It also provides excellent moisture and gas barrier properties. This prevents premature oxidation and dehydration, extending the shelf life of highly perishable goods.
Most buyers recognize PET by the Resin Identification Code (RIC) #1 stamped on the bottom of the container. A widespread misconception persists regarding this symbol. The RIC #1 does not guarantee a local municipality will accept or successfully recycle the item. It serves purely as a regulatory and sorting identifier for the polymer type. It tells material recovery facilities exactly what chemical compound they are handling. The facility's mechanical capabilities ultimately determine if they recover that polymer.
When evaluating material sourcing, you must understand the distinction between virgin PET and post-consumer recycled PET (rPET). Virgin PET comes directly from petrochemical feedstocks. It offers pristine structural integrity and maximum clarity. In contrast, manufacturers produce rPET from recovered plastics that facilities have washed, melted, and re-pelletized. Historically, rPET suffered from slight yellowing or structural brittleness. Today, advanced super-cleaning technologies and solid-state polycondensation processes restore rPET to near-virgin quality. These advancements ensure high-percentage rPET containers maintain strict food-grade safety standards.
The color of the polymer dictates its end-of-life viability. Modern recycling centers rely on Near-Infrared (NIR) optical sorting technology. These machines identify and separate different plastics at high speeds on a conveyor belt. Clear PET reflects the NIR light perfectly. The sensors identify the polymer signature and blast it into the correct recycling stream with an air jet. Conversely, black PET absorbs the NIR light. Manufacturers often color it using carbon black pigments. Because the optical sorter receives no reflected signal, the black plastic remains invisible to the system. The facility misidentifies these containers as residual waste and routes them directly to landfills.
To understand true recyclability, look at the mechanical recycling process at municipal Material Recovery Facilities (MRFs). When mixed recyclables arrive, they undergo a complex sorting sequence.
Despite this infrastructure, the thermoform challenge remains a massive technical hurdle. We must distinguish between PET bottles (blow-molded) and PET thermoforms (like a standard produce container). Blow-molded bottles have a higher intrinsic viscosity. Their polymer chains are longer and more robust. Thermoformed containers have a lower intrinsic viscosity and melt at slightly different temperatures. When facilities mix thermoform flakes with bottle flakes in high concentrations, they alter the melting characteristics of the batch. This causes processing issues for downstream recyclers. Many MRFs explicitly accept PET bottles but reject PET thermoforms to protect their primary bottle-grade rPET bales.
Contamination represents another major roadblock. Organic matter like sticky fruit juice, mold, or decaying plant material severely impacts washing protocols. Hot wash lines handle minor residues, but excessive contamination ruins entire batches of recycled flake. If a bale of recovered PET exceeds the facility's strict threshold for organic contamination, they downgrade or reject the entire bale. It goes straight to the landfill. Designing packaging that minimizes liquid pooling and encourages consumers to rinse the container improves actual recovery rates.
The end-market for recovered PET dictates whether the process is truly circular. Closed-loop recycling happens when a recovered food container becomes another food-grade container. Bottle-to-bottle or tray-to-tray recycling is the gold standard. However, a significant portion of recovered PET undergoes downcycling. Facilities convert the material into secondary products like polyester carpet fibers, clothing, or industrial strapping. Downcycling diverts plastic from landfills temporarily, but it removes the polymer from the closed-loop food packaging supply chain. This forces the continuous extraction of virgin fossil fuels to create new food containers.
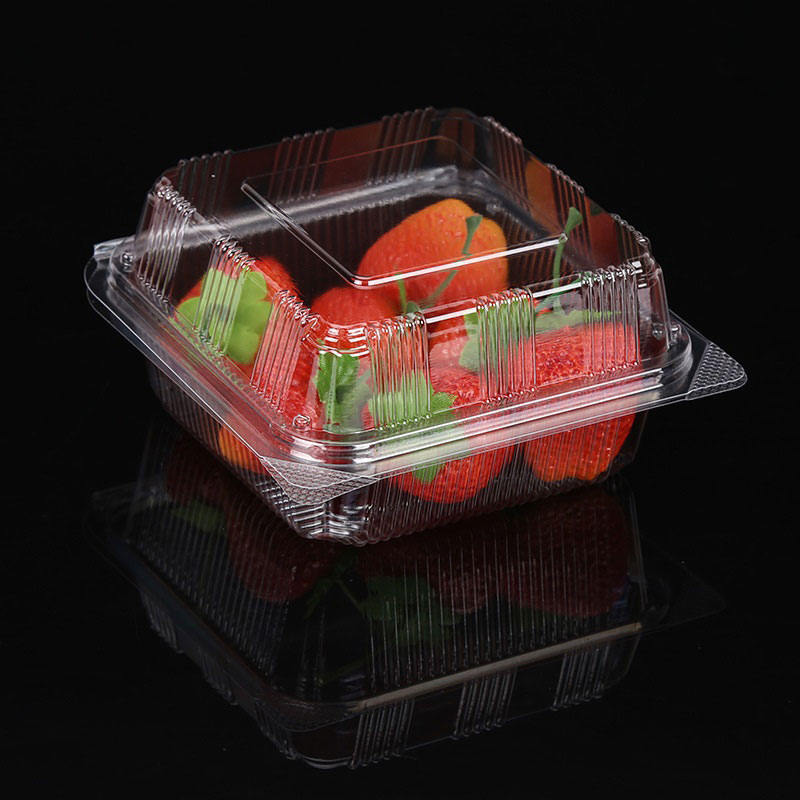
The baseline recyclability of a standard rectangular plastic fruit box is generally high, provided you manufacture it from clear, mono-material PET. These containers dominate the agricultural sector due to predictable dimensions and reliable performance. Because they are clear, they pass through NIR optical sorters with minimal issues, assuming the local MRF accepts thermoformed PET.
The physical design directly impacts transit efficiency and sorting viability. You must calibrate wall thickness carefully during the extrusion process. Walls that are too thin crush under pallet weight. Excessively thick walls increase material usage and environmental footprint. Rigid designs with built-in nesting capabilities allow empty containers to stack tightly. This drastically reduces outbound freight emissions by maximizing trailer space. At the recycling facility, rigid walls help the container maintain its 3D shape on the conveyor belt. This makes it easier for optical sorters to identify and eject the item. Flimsy containers flatten easily and get mis-sorted as 2D paper or film waste.
Geometric design plays a massive role in protecting high-value produce. An octagonal fruit tray utilizes angled corners to significantly improve crush resistance and load-bearing capacity during palletized transit. The octagonal structure distributes vertical weight more evenly than standard 90-degree corners. This reduces the risk of bottom-tier collapse when you stack pallets high in distribution centers.
Complex geometries require careful evaluation regarding end-of-life processing. The internal angles and structural ribs of an octagonal design trap more food residue. Sticky berry juice or grape stems get stuck in the crevices compared to smooth-walled containers. If consumers fail to rinse these complex trays adequately, the trapped residue complicates the washing phase during mechanical recycling. Packaging engineers must balance the structural benefits of complex geometries with the necessity of easy cleaning. This ensures the tray remains a viable candidate for closed-loop recycling.
Fresh berries are highly sensitive to their micro-environment. Ventilation is a non-negotiable feature. A strawberry clamshell box requires precise ventilation holes to allow for ethylene gas release and proper moisture control. Without these vents, condensation builds up rapidly. This leads to accelerated mold growth and massive product loss. These physical cuts affect the thermoforming process. You need specialized tooling to punch the holes without weakening the surrounding polymer structure.
Beyond ventilation, labels and adhesives have the most significant impact on recyclability. A perfectly clear PET clamshell becomes entirely unrecyclable if you cover it in a large paper label applied with a permanent, non-water-soluble adhesive. During the float-sink process, incompatible adhesives cause paper fibers and ink to bind to the PET flakes. This contaminates the batch. Procurement teams must specify wash-away adhesives and PET-compatible labels. These specialized components detach cleanly in the hot wash line, allowing facilities to recover the pure PET flake successfully.
The lifecycle of a disposable fruit box dictates its ultimate disposal route. Consumers frequently use these containers for on-the-go consumption. You see them holding pre-cut fruit in convenience stores, airports, or corporate cafeterias. Because people consume the contents away from home, they often toss the packaging into public trash bins rather than dedicated recycling receptacles.
Consumer behavior heavily influences the actual recovery rate of these convenience containers. Even when placed in a recycling bin, on-the-go containers are rarely rinsed. The residual sugars and organic matter left inside attract pests. They also contaminate surrounding paper products in single-stream recycling systems. Addressing this single-use reality requires clear, actionable labeling. You must educate the consumer on proper disposal while supporting municipal investments in public recycling infrastructure that handles higher contamination thresholds.
Selecting the optimal Plastic Box requires a structured procurement framework. You must align physical packaging features with desired business outcomes. The baseline requirements for any food packaging include extending shelf-life, preventing transit damage, and maximizing retail visibility. Modern procurement must also satisfy the rigorous sustainability scorecards implemented by major retail chains. Failing to meet these scorecards results in delisting or reduced shelf space.
Buyers must compare PET against alternative materials using a strict performance matrix.
| Material Type | Clarity & Visibility | Moisture/Gas Barrier | Recycling Infrastructure | Primary Drawbacks |
|---|---|---|---|---|
| PET / rPET | Excellent (High Transparency) | High | Widely established globally | Thermoform sorting challenges at some local MRFs. |
| Polypropylene (PP) | Moderate (Slightly Hazy) | Moderate | Growing, but less universal than PET | Lower clarity reduces fresh produce appeal. |
| Polylactic Acid (PLA) | High | Low to Moderate | Requires industrial composting | Acts as a severe contaminant if mixed into PET recycling streams. |
| Molded Fiber | Opaque (Zero Visibility) | Low (Requires synthetic liners) | Highly sustainable/compostable | Cannot showcase fresh produce; absorbs moisture from fruit. |
Compliance with emerging Extended Producer Responsibility (EPR) legislation fundamentally alters procurement strategies in North America and Europe. EPR laws shift the financial burden of end-of-life disposal away from municipalities and back to the manufacturer or distributor. Packaging that is difficult to recycle, heavily pigmented, or made from multi-material laminates incurs significantly higher EPR fees and plastic taxes. Highly recyclable, mono-material PET designs benefit from lower regulatory fees. This makes them a more economically viable choice over the long term.
When evaluating cost-to-value trade-offs, weigh the unit economics of virgin PET against alternative materials. Molded fiber or PLA might align with certain marketing narratives, but their hidden costs are substantial. The lower moisture barrier of molded fiber reduces the shelf life of berries by several days. This leads to increased food waste at the retail level. The financial loss from spoiled produce far outweighs the fractional savings on the packaging unit price.
To ensure compliance and performance, procurement teams should utilize a strict supplier vetting checklist. Ask potential packaging partners these actionable questions:
Transitioning to highly recyclable or rPET-based packaging introduces specific operational risks. You must manage these proactively. The first major risk involves supply chain vulnerabilities associated with rPET sourcing. A global market shortage of high-quality, food-grade rPET currently exists, driven by massive demand from beverage conglomerates. This shortage leads to severe price volatility and delayed shipments. To mitigate this risk, diversify your supplier networks rather than relying on a single vendor. Lock in long-term contracts for recycled resin and consider hybrid blends. A guaranteed 30% rPET mixed with virgin PET stabilizes supply lines while still meeting baseline sustainability targets.
Food safety and regulatory non-compliance represent a major risk, particularly regarding chemical migration. When using recycled materials, a theoretical risk exists that legacy contaminants from the post-consumer waste stream could migrate into fresh food. Mitigating this risk requires absolute strictness in documentation. Demand FDA Letters of No Objection (LNO) or European Food Safety Authority (EFSA) approvals from your suppliers. These documents legally certify that the super-cleaning processes used to manufacture the rPET remove all volatile organic compounds and ensure safety for direct food contact.
Greenwashing and consumer backlash pose significant legal and reputational risks. Labeling a product as "100% Recyclable" triggers regulatory fines or class-action lawsuits in regions where thermoform recycling is technically unavailable. The Federal Trade Commission (FTC) Green Guides strictly regulate how brands market environmental claims. Adopt standardized, transparent labeling systems, such as the How2Recycle program. These systems provide accurate, localized disposal instructions based on current municipal capabilities. This protects your brand from false advertising claims.
Adhesive and component incompatibility ruins otherwise perfect packaging initiatives. An entirely recyclable clear PET container becomes landfill waste if you utilize permanent rubber-based adhesives or incompatible absorbent pads glued to the base. Recyclers cannot separate these materials efficiently. Mandate mono-material designs in all supplier contracts. If you need absorbent pads for moisture control, ensure they are friction-fitted rather than glued. Vet all labels and adhesives against APR guidelines to ensure they wash away cleanly during the mechanical recycling process.
To build a resilient and compliant packaging strategy, execute the following steps immediately:
A: Standard PET is not microwave safe. It has a low heat tolerance and will warp, melt, or potentially leach chemicals into food when exposed to microwave temperatures. For microwave applications, you must use packaging made from CPET (Crystallized PET) or Polypropylene (PP). Engineers design these materials specifically to withstand high heat without degrading.
A: Yes. Removing organic residue is critical. Leftover fruit juice, mold, or food particles contaminate the washing lines at the Material Recovery Facility (MRF). If a batch of recyclables exceeds the facility's strict contamination threshold, they will reject the entire bale and send it directly to a landfill.
A: PET bottles are blow-molded and have a higher intrinsic viscosity, meaning their polymer chains are longer and stronger. Fruit boxes are thermoformed, giving them a lower intrinsic viscosity and a different melting point. Mixing too many thermoforms with bottles disrupts the recycling process for high-grade bottle resin.
A: Yes, manufacturing a clamshell from 100% rPET is technically feasible. However, it requires advanced super-cleaning technologies to meet strict FDA and EFSA food-contact requirements. Because 100% rPET sometimes exhibits slight brittleness or a faint color tint, many brands opt for a 30% to 50% blend with virgin PET.
A: Recycling facilities use Near-Infrared (NIR) optical sorters to identify plastic types. The carbon black pigment used in black plastics absorbs the NIR light instead of reflecting it. Because the scanner cannot read the polymer signature, the system assumes it is residual waste and routes it to the landfill.
A: No. Manufacturers typically make absorbent pads from a mix of paper, super-absorbent polymers, and plastic films. They are multi-material components that severely contaminate the PET recycling stream. Consumers must remove them and throw them in the trash before placing the tray in the recycling bin.


